Electrical Discharge Machining (EDM)
We operate a Suzhou Baoma BM500 closed-loop EDM wire cutting machine capable of ±0.0025 mm accuracy. EDM uses spark erosion to perform non-contact cuts, making it ideal for intricate geometries, thin-walled sections, exotic metals, and components where conventional machining introduces unacceptable force or heat.
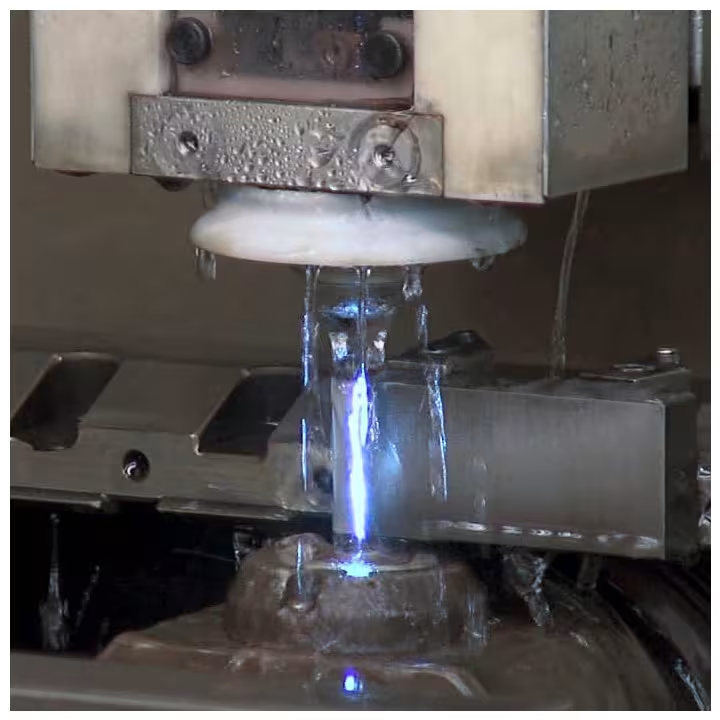
EDM wire cutting removes material using a controlled electrical discharge, a timed spark that arcs between a thin wire electrode (typically brass or molybdenum, around 0.025 mm diameter) and the workpiece. The spark occurs thousands of times per second, eroding material along a precisely programmed path. A jet of deionised water acts as both a dielectric medium and a means of flushing away metal particles only microns in diameter. Because the wire never physically contacts the workpiece, the process applies no cutting force and introduces negligible heat. This makes EDM uniquely suited to parts that would deform, burr, or fracture under conventional machining.
Precision Without Compromise
EDM is not a substitute for conventional machining, instead it solves problems that conventional machining cannot. When a part requires sub-micron surface finish in hardened tool steel, or an L-shaped internal cavity in a titanium housing, EDM is often the only viable process. APAC's CNC-controlled Baoma BM500 accepts direct 2D and 3D CAD input, eliminating manual programming errors and enabling fast turnaround from design file to finished part.
If your component involves tight tolerances, exotic materials, or geometries that conventional cutting tools struggle with, EDM is likely the answer. Send us your CAD files or get in touch to discuss your requirements.
When to Use EDM
- Very thin-walled material - no force, no deformation
- Non-round cavities and openings where rotating tools can't reach
- Recessed and internal cuts beyond conventional tool access
- Angled and 3D orbital cuts
- Materials that burr or produce hazardous dust under conventional machining
Materials & Applications
- Hardened steels, tool steels, stainless steels
- Tungsten carbide, titanium, and exotic alloys
- Fragile or thin-section components
- Injection mould tooling and die components
- Defence, aerospace, and precision instrument parts
Equipment & Specifications
- Suzhou Baoma BM500 closed-loop EDM wire cut
- Wire diameter: typically 0.025 mm
- Positional accuracy: ±0.0025 mm
- CNC-controlled from 2D DXF or 3D model data
- Brass and molybdenum wire electrodes